TECHNICAL GUIDE / 2026-10-03
Short answer. Choose brown fused alumina grit for cast iron cleaning by the amount of adhered sand, scale or coating to remove and the finish required afterward. Qualify the media on representative castings, including recesses and machined faces.
Define the job before naming the abrasive
Castings from different molds and cleaning histories can arrive with very different surfaces. Distinguish adhered molding sand from rust, paint and machining coolant residue. Specify which surfaces may be blasted and which must be protected. A cast iron housing with a seal face requires different masking from a decorative casting. If coating follows, include its cleanliness and profile requirements in the cleaning plan.
Write the requirement as an observable result. Identify the incoming workpiece or formulation, the stage at which the abrasive is used, and the step that follows. Agree on how a pass and a failure will be measured. The same material may be suitable for one stage and unsuitable for another because the geometry, process medium or acceptance rule changes. A supplier can help narrow grades, but the processor owns the operating conditions and finished result. If a drawing or customer procedure already controls the choice, bring that document into the trial plan.
Compare delivered grades, not just material names
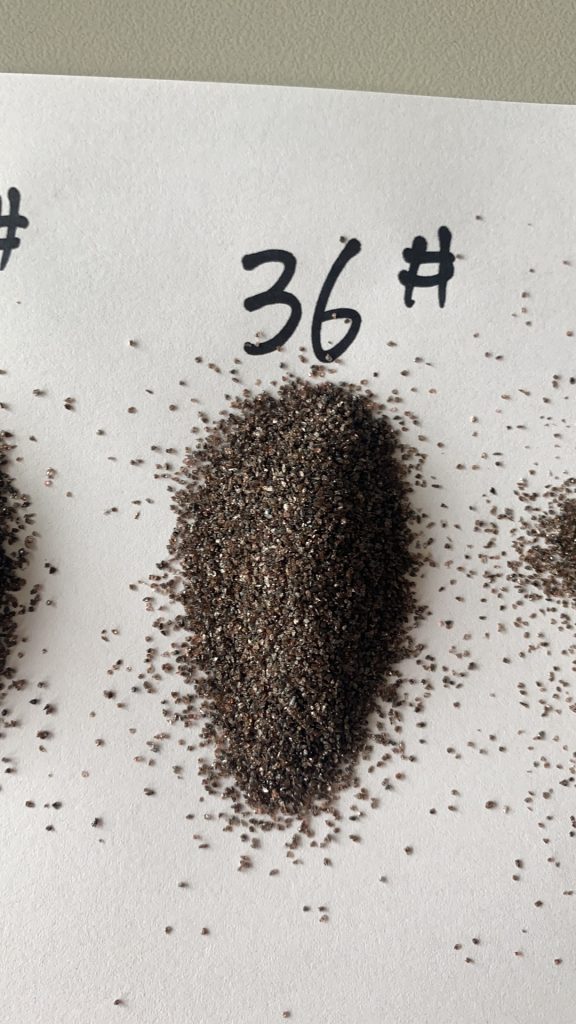
Compare a practical range of brown fused alumina F grades under the actual blast equipment. A larger particle can alter impact and texture, but it may not reach narrow recesses as the process expects. A smaller grain may require different exposure to remove stubborn deposits. Request the supplied distribution and examine fines from reclaimed media. The grade should be selected with pressure, nozzle, feed rate and recovery system rather than by a chart alone.
Use the offered batch or a representative retained sample. Ask how size distribution was measured, what grade designation applies and whether the information is typical product data or a batch-specific test. Nominal size is useful for screening but does not describe every particle in a delivery. Compare the data with the existing approved input, including fines and oversize where they matter. Keep product family, grain grade and the finished tool or mix specification as separate records; confusing them makes a later purchase order hard to repeat.
Build a trial that isolates the decision
Select parts with typical and difficult features. Record the incoming condition and photograph several marked zones. Run matched settings for candidate grades and measure cleaning completeness, profile and time. Inspect around bolt holes, ribs and protected machined surfaces. If the media will be reused, test the normal recovery cycle and screen condition; a fresh-media-only comparison may not represent production.
Record the baseline before introducing a substitute. Use comparable parts or batches and hold the main machine and formulation variables steady in the first round. Mark every sample with the abrasive lot, date and run conditions. If the comparison exposes a promising candidate, optimize its process settings in a separate round. This sequence prevents a simultaneous change in media, pressure, feed or binder from being credited to the wrong cause. Include normal equipment wear and reclaimed media only when those conditions are part of production.
Inspect both the result and the next operation
Look for remaining embedded sand, excessive roughness, exposed porosity and accidental removal of a protective surface. Clean the casting as it will be cleaned before painting or assembly, then inspect again for trapped particles. Track dust loading and filter service as operational outcomes. A single clean photograph is insufficient if hidden passages or gasket faces remain contaminated.
Define the inspection method before seeing the samples. Look at average performance and localized failures such as corners, edges, recesses or individual deep marks. If another operation follows, carry the trial through that step because a clean intermediate surface can still cause downstream rework. Record consumption, yield and handling alongside technical measurements. A faster pass is not automatically economical when it raises scrap, tool replacement or cleaning time. Retain rejected and accepted samples for a review with the processor and supplier.
Make the buying specification reproducible
The order should name F grade, acceptable distribution, packaging, lot traceability and any contamination limits. Provide the supplier with cast iron type, cleaning target and reuse plan. Retain a sample of the approved abrasive and a reference casting. Changes in foundry sand, blast machine or downstream coating require a fresh check.
Keep an approved sample, the supplier's product data sheet, the applicable batch report and the internal trial record together. A product sheet describes a supply range; it is not evidence that every shipment or finished part has a particular performance. State the order of precedence if purchase text, drawing and trial approval differ. At receipt, compare the delivered label and batch paperwork with the approved description. Hold an unapproved substitution for review rather than relying on a similar-looking material name.
Close the loop after a successful trial
Once a candidate passes, document exactly which conditions made the decision valid: the material family, grade, size method, supplier lot, equipment or formulation revision, inspection method and downstream step. Tell production and purchasing which changes require a repeat trial. A later problem can then be traced to a controlled difference instead of debated from memory. If the intended use is outside the tested window, obtain a new sample and repeat the relevant checks. This is particularly important when a raw abrasive is incorporated into a wheel, belt, refractory mix or coating preparation process, where the finished result depends on several organizations.
Selection guidance
Start with the current approved grade or process as a reference. Ask for one or two candidate lots that meet the written input limits, and compare them on representative work. Rank each candidate against the actual acceptance rule, then consider operating cost and supply consistency. A laboratory measurement can help explain a result but should not replace the finished-part or finished-mix trial. If no candidate passes, revise the process question or equipment setup before widening material choices. For cast iron surface cleaning, retain the control sample and the test conditions used to approve it.
Common mistakes
- Choosing from the abrasive family name without an agreed grade and batch report.
- Changing several process settings during the first material comparison.
- Approving a visually acceptable sample without the required downstream check.
- Losing the connection between the tested lot and the repeat purchase order.
Related technical guidance
Frequently asked questions
Can a nominal grit number alone settle this selection?
No. It screens possible candidates, but the delivered distribution, machine or formulation and finished-result test decide whether the material fits. Use the applicable F, P or refractory grain designation and confirm the measurement method with the supplier.
When should the trial be repeated?
Repeat the affected checks when the input grade or supplier lot characteristics, equipment, binder, workpiece or acceptance requirement changes beyond the approved window. The change record should say which prior evidence remains applicable and which result needs fresh verification.